Uploaded January 2026 | Updated September 2026, 2 weeks ago
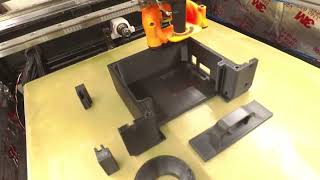
I set up a profile for functional prints today. I didn't want it to be artifact ridden and needed an Orca profile I can work with.
Gridfinity: printables.com/model/543553-gridfinity-storage-box-by-pred-now-parametric
This has a flow cap of 60mms3, ABS, Orange Likeisilk, 315C(would not flow below 300C @ 60mms3).
0.4TC nozzle, 0.3 layer height, 62mms3 max flow
20-60K acceleration, 10-40SCV, 200-250mms overhang, 200mms 1st layer, PA 0.01, ST .02 - main box
1:42:48 print time
60K accel, 800mms, 60SCV, 1x1 box, 0.3 layer height, 0.5 line width, 6:37
This is not a "haul ballz' print, but one that is producing excellent prints.
It took 3 tries to get this, from watching infill placement to top layers at max flow (different brand filament, new to me, needs more temp than typical ABS)
What is for sure, we need more flow. Can't really use more speed without the flow and I am not into CHT from past experience. Time for a dual lane hotend!
Also, if flow is on the cusp, typical PA is not working. For high speed infill/solid tops, PA .005. But for walls and seams, .01PA .02ST. Can see some smearing of the seams at higher PA and this flow point. Slicers need to implement variable PA, it works!
I set up a profile for functional prints today. I didn't want it to be artifact ridden and needed an Orca profile I can work with.
Gridfinity: printables.com/model/543553-gridfinity-storage-box-by-pred-now-parametric
This has a flow cap of 60mms3, ABS, Orange Likeisilk, 315C(would not flow below 300C @ 60mms3).
0.4TC nozzle, 0.3 layer height, 62mms3 max flow
20-60K acceleration, 10-40SCV, 200-250mms overhang, 200mms 1st layer, PA 0.01, ST .02 - main box
1:42:48 print time
60K accel, 800mms, 60SCV, 1x1 box, 0.3 layer height, 0.5 line width, 6:37
This is not a "haul ballz' print, but one that is producing excellent prints.
It took 3 tries to get this, from watching infill placement to top layers at max flow (different brand filament, new to me, needs more temp than typical ABS)
What is for sure, we need more flow. Can't really use more speed without the flow and I am not into CHT from past experience. Time for a dual lane hotend!
Also, if flow is on the cusp, typical PA is not working. For high speed infill/solid tops, PA .005. But for walls and seams, .01PA .02ST. Can see some smearing of the seams at higher PA and this flow point. Slicers need to implement variable PA, it works!