Uploaded October 2026 | Updated November 2026, 1 day ago
PLC start stop jog in structured text, line by line: X1 start, the Y1 AND NOT C1 seal-in, X3 jog, X2 stop normally closed, and why C1 stops jog latching.
⚡ QUICK ANSWER
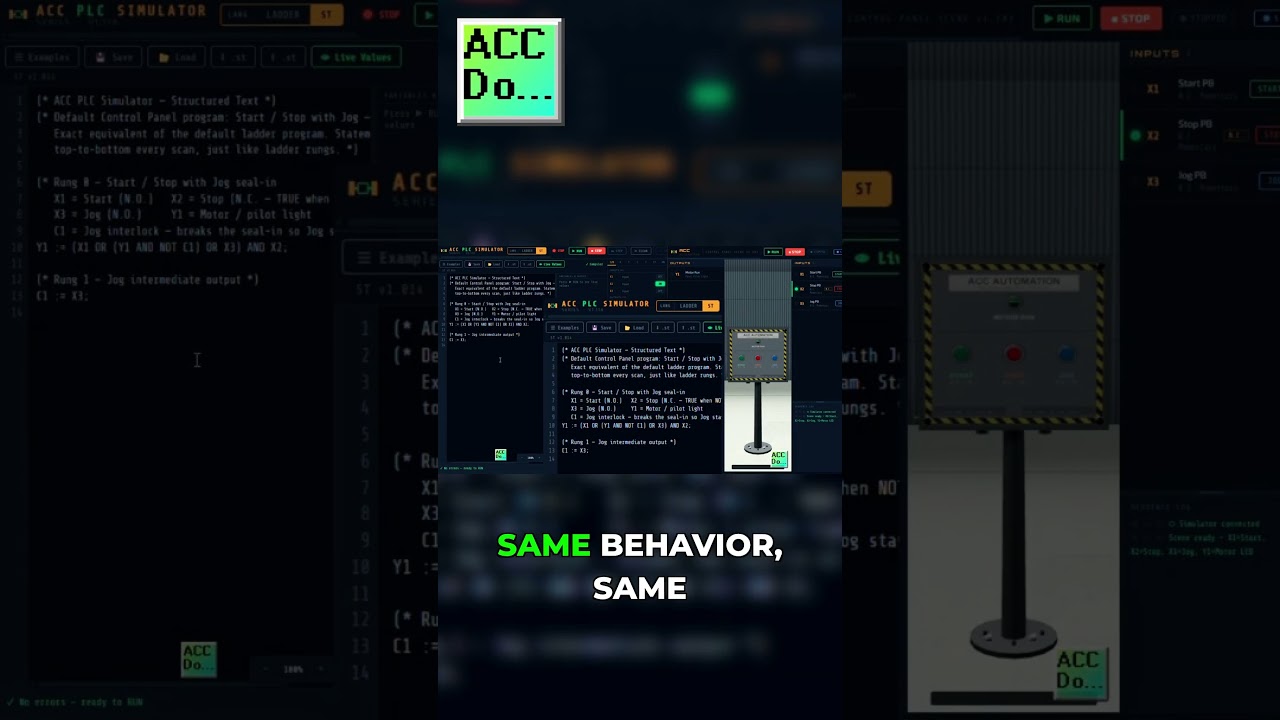
The whole circuit is two lines:
Y1 := (X1 OR (Y1 AND NOT C1) OR X3) AND X2;
C1 := X3;
X1 is start. Y1 AND NOT C1 is the seal-in - it keeps the motor running after you release start, but only while C1 is false. X3 is jog. All three feed into AND X2, and X2 is a normally closed stop button, so it reads TRUE at rest and the expression passes; press stop and it goes false and the output drops. The second line is the trick: C1 := X3 means pressing jog sets C1, which breaks the seal-in branch. So jog drives the output directly while it is held, and nothing latches it on when you let go - no one shot and no separate interlock rung needed. Same addresses, same behaviour and same I/O as the ladder version. Full guide on the blog.
📖 FULL WRITTEN GUIDE
accautomation.ca/acc-plc-simulator-how-to-use-structured-text-st-programming
🖥️ OPEN THE SIMULATOR AND PRESS ST
accautomation.ca/simulator
▶ WATCH THE FULL VIDEO
youtu.be/B0UDgJnE3DQ
📚 WHAT YOU'LL LEARN
✅ Read a seal-in circuit as a single expression - Y1 AND NOT C1 is the branch that holds the output on after start is released
✅ Understand why the stop button is ANDed in rather than inverted - X2 is a normally closed field device, so it reads TRUE at rest and FALSE when pressed
✅ See how jog avoids latching - X3 feeds the output directly, and C1 := X3 breaks the seal-in branch at the same time
✅ Write a complete start, stop and jog motor circuit in two lines, with no one shot and no extra interlock rung
✅ Compare it against the ladder version using the same X, Y and C addresses in the same simulator
❓ FREQUENTLY ASKED
Q: What is a seal-in circuit?
A: The branch that keeps an output on after the start button is released. Here it is Y1 AND NOT C1 - the output feeding back into its own condition, which is the text version of the holding contact you would wire around a start pushbutton in ladder.
Q: Why is the stop button ANDed instead of inverted?
A: Because a stop button is wired normally closed, so the input is TRUE when nothing is pressed. ANDing it means the circuit runs normally and drops out the moment the contact opens - including if a wire breaks, which is the whole point of wiring stop normally closed.
Q: Why does jog need C1 at all?
A: Without it, jog would feed the seal-in and the motor would stay running after you released the jog button. C1 := X3 breaks the seal-in branch while jog is pressed, so the output follows the button and releases cleanly.
👉 The full guide, with every statement and function block: accautomation.ca/acc-plc-simulator-how-to-use-structured-text-st-programming
🔗 MORE RESOURCES
▶ Try the free simulator: accautomation.ca/simulator
▶ How I learned structured text in the simulator: youtu.be/B0UDgJnE3DQ
▶ Why a stop button is wired normally closed: youtube.com/shorts/wCgr-ZzG_J0
▶ PLC Beginners Guide: accautomation.ca/programming/plc-beginners-guide
▶ Free eBooks: accautomation.ca (subscribe for download)
🛒 RECOMMENDED HARDWARE
▶ Shop: automationdirect.com
▶ Parts Guide: accautomation.ca/purchase-find-parts
💬 Questions? Drop a comment below.
🔔 New tutorials every Monday — Subscribe and hit the bell!
#PLC #LadderLogic #IndustrialAutomation #PLCProgramming #ACCAutomation #StructuredText #IEC61131 #MotorControl #LearnPLC #Shorts
Regards,
Garry
ACC Automation
accautomation.ca
PLC start stop jog in structured text, line by line: X1 start, the Y1 AND NOT C1 seal-in, X3 jog, X2 stop normally closed, and why C1 stops jog latching.
⚡ QUICK ANSWER
The whole circuit is two lines:
Y1 := (X1 OR (Y1 AND NOT C1) OR X3) AND X2;
C1 := X3;
X1 is start. Y1 AND NOT C1 is the seal-in - it keeps the motor running after you release start, but only while C1 is false. X3 is jog. All three feed into AND X2, and X2 is a normally closed stop button, so it reads TRUE at rest and the expression passes; press stop and it goes false and the output drops. The second line is the trick: C1 := X3 means pressing jog sets C1, which breaks the seal-in branch. So jog drives the output directly while it is held, and nothing latches it on when you let go - no one shot and no separate interlock rung needed. Same addresses, same behaviour and same I/O as the ladder version. Full guide on the blog.
📖 FULL WRITTEN GUIDE
accautomation.ca/acc-plc-simulator-how-to-use-structured-text-st-programming
🖥️ OPEN THE SIMULATOR AND PRESS ST
accautomation.ca/simulator
▶ WATCH THE FULL VIDEO
youtu.be/B0UDgJnE3DQ
📚 WHAT YOU'LL LEARN
✅ Read a seal-in circuit as a single expression - Y1 AND NOT C1 is the branch that holds the output on after start is released
✅ Understand why the stop button is ANDed in rather than inverted - X2 is a normally closed field device, so it reads TRUE at rest and FALSE when pressed
✅ See how jog avoids latching - X3 feeds the output directly, and C1 := X3 breaks the seal-in branch at the same time
✅ Write a complete start, stop and jog motor circuit in two lines, with no one shot and no extra interlock rung
✅ Compare it against the ladder version using the same X, Y and C addresses in the same simulator
❓ FREQUENTLY ASKED
Q: What is a seal-in circuit?
A: The branch that keeps an output on after the start button is released. Here it is Y1 AND NOT C1 - the output feeding back into its own condition, which is the text version of the holding contact you would wire around a start pushbutton in ladder.
Q: Why is the stop button ANDed instead of inverted?
A: Because a stop button is wired normally closed, so the input is TRUE when nothing is pressed. ANDing it means the circuit runs normally and drops out the moment the contact opens - including if a wire breaks, which is the whole point of wiring stop normally closed.
Q: Why does jog need C1 at all?
A: Without it, jog would feed the seal-in and the motor would stay running after you released the jog button. C1 := X3 breaks the seal-in branch while jog is pressed, so the output follows the button and releases cleanly.
👉 The full guide, with every statement and function block: accautomation.ca/acc-plc-simulator-how-to-use-structured-text-st-programming
🔗 MORE RESOURCES
▶ Try the free simulator: accautomation.ca/simulator
▶ How I learned structured text in the simulator: youtu.be/B0UDgJnE3DQ
▶ Why a stop button is wired normally closed: youtube.com/shorts/wCgr-ZzG_J0
▶ PLC Beginners Guide: accautomation.ca/programming/plc-beginners-guide
▶ Free eBooks: accautomation.ca (subscribe for download)
🛒 RECOMMENDED HARDWARE
▶ Shop: automationdirect.com
▶ Parts Guide: accautomation.ca/purchase-find-parts
💬 Questions? Drop a comment below.
🔔 New tutorials every Monday — Subscribe and hit the bell!
#PLC #LadderLogic #IndustrialAutomation #PLCProgramming #ACCAutomation #StructuredText #IEC61131 #MotorControl #LearnPLC #Shorts
Regards,
Garry
ACC Automation
accautomation.ca