Uploaded November 2026 | Updated November 2026, 1 day ago
PLC code that passes every test can still be wrong. Trace the scan order, the NOT X2 logic and variable initialization before you trust AI generated logic.
⚡ QUICK ANSWER
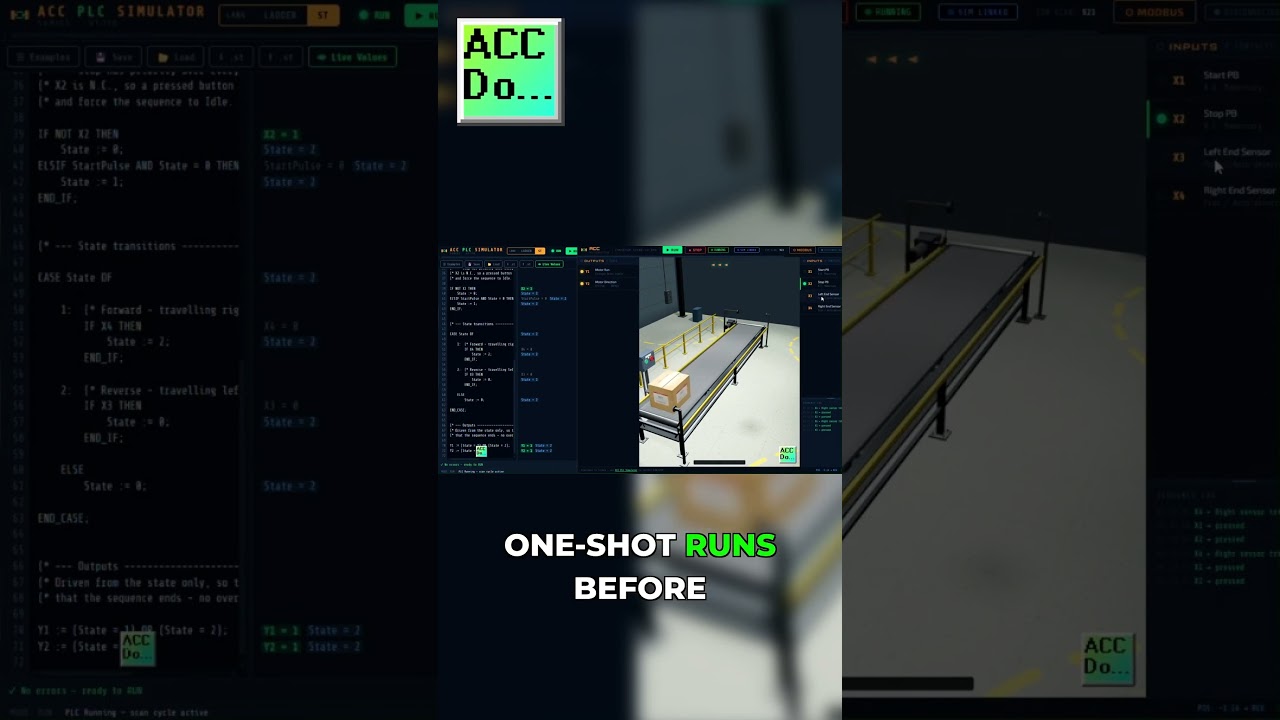
PLC scan order decides whether correct looking Structured Text actually behaves correctly, so passing every functional test is not proof. Twenty minutes in step mode confirmed the real execution order in this conveyor program: the one shot runs first, then the stop check, then the CASE transitions, then the outputs. A reviewer also has to know why NOT X2 means the stop button is pressed, and has to check how every variable initializes. That last check turned up one edge case, and the written test walks through it.
📖 FULL STEP-BY-STEP + DOWNLOADS (project file, wiring diagrams, screenshots)
accautomation.ca/can-ai-program-a-plc-i-tested-it-live-in-the-acc-plc-simulator
📚 WHAT YOU'LL LEARN
✅ Step a PLC program one scan at a time to confirm the real execution order
✅ Check that a one shot fires before the logic that depends on it, not after
✅ Read NOT X2 correctly when X2 is a normally closed stop that is TRUE at rest
✅ Audit variable initialization to catch the first scan edge cases tests miss
✅ Review AI generated PLC code as code, not as a black box that passed
❓ FREQUENTLY ASKED
Q: Why does NOT X2 mean the stop button is pressed?
A: X2 is a normally closed stop, so it reads TRUE while at rest. The contact only opens when the button is pressed, which makes NOT X2 the condition that means stop.
Q: If every test passed, what is left to check?
A: Scan order and initialization. Logic can produce the right outputs during a normal run and still misfire on the first scan or when two conditions land in the same scan.
Q: What is step mode used for here?
A: Running one scan at a time so you can watch which block executes before which, instead of assuming the order the code is written in is the order it runs.
👉 Full step-by-step, code and wiring diagrams: accautomation.ca/can-ai-program-a-plc-i-tested-it-live-in-the-acc-plc-simulator
🔗 MORE RESOURCES
▶ Series: accautomation.ca/series
▶ Free PLC Simulator: accautomation.ca/simulator
▶ PLC Beginners Guide: accautomation.ca/programming/plc-beginners-guide
▶ Free eBooks: accautomation.ca (subscribe for download)
🛒 RECOMMENDED HARDWARE
▶ Shop: automationdirect.com
▶ Parts Guide: accautomation.ca/purchase-find-parts
💬 Questions? Drop a comment below.
🔔 New tutorials every Monday — Subscribe and hit the bell!
#PLC #StructuredText #IndustrialAutomation #PLCProgramming #ACCAutomation #PLCTutorial #LearnPLC #Shorts
Regards,
Garry
ACC Automation
accautomation.ca
PLC code that passes every test can still be wrong. Trace the scan order, the NOT X2 logic and variable initialization before you trust AI generated logic.
⚡ QUICK ANSWER
PLC scan order decides whether correct looking Structured Text actually behaves correctly, so passing every functional test is not proof. Twenty minutes in step mode confirmed the real execution order in this conveyor program: the one shot runs first, then the stop check, then the CASE transitions, then the outputs. A reviewer also has to know why NOT X2 means the stop button is pressed, and has to check how every variable initializes. That last check turned up one edge case, and the written test walks through it.
📖 FULL STEP-BY-STEP + DOWNLOADS (project file, wiring diagrams, screenshots)
accautomation.ca/can-ai-program-a-plc-i-tested-it-live-in-the-acc-plc-simulator
📚 WHAT YOU'LL LEARN
✅ Step a PLC program one scan at a time to confirm the real execution order
✅ Check that a one shot fires before the logic that depends on it, not after
✅ Read NOT X2 correctly when X2 is a normally closed stop that is TRUE at rest
✅ Audit variable initialization to catch the first scan edge cases tests miss
✅ Review AI generated PLC code as code, not as a black box that passed
❓ FREQUENTLY ASKED
Q: Why does NOT X2 mean the stop button is pressed?
A: X2 is a normally closed stop, so it reads TRUE while at rest. The contact only opens when the button is pressed, which makes NOT X2 the condition that means stop.
Q: If every test passed, what is left to check?
A: Scan order and initialization. Logic can produce the right outputs during a normal run and still misfire on the first scan or when two conditions land in the same scan.
Q: What is step mode used for here?
A: Running one scan at a time so you can watch which block executes before which, instead of assuming the order the code is written in is the order it runs.
👉 Full step-by-step, code and wiring diagrams: accautomation.ca/can-ai-program-a-plc-i-tested-it-live-in-the-acc-plc-simulator
🔗 MORE RESOURCES
▶ Series: accautomation.ca/series
▶ Free PLC Simulator: accautomation.ca/simulator
▶ PLC Beginners Guide: accautomation.ca/programming/plc-beginners-guide
▶ Free eBooks: accautomation.ca (subscribe for download)
🛒 RECOMMENDED HARDWARE
▶ Shop: automationdirect.com
▶ Parts Guide: accautomation.ca/purchase-find-parts
💬 Questions? Drop a comment below.
🔔 New tutorials every Monday — Subscribe and hit the bell!
#PLC #StructuredText #IndustrialAutomation #PLCProgramming #ACCAutomation #PLCTutorial #LearnPLC #Shorts
Regards,
Garry
ACC Automation
accautomation.ca