Uploaded January 2016 | Updated September 2026, 1 week ago
NEW CONFIGURABLE NAAMS COMPONENTS FROM MISUMI USA!
youtube.com/watch?v=FYi48fVdGfA
-~-~~-~~~-~~-~-
Locating Pins Pt. 4: Alignment Concerns | Engineer to Engineer | MISUMI USA
misumiusa.com
When working with and designing jigs or fixtures with locating pins, proper alignment is crucial to ensuring smooth operation and repeatable results. This episode will address a few of the most common solutions to alignment concerns for locating pins. If you're unfamiliar with the basics of locating pins and workholding concepts, check out the previous episodes in this series to get up to speed.
One of the biggest issues a new fixture designer encounters is binding of a part, where the way it is placed or removed from a pair of locating pins causes it to become stuck and out of alignment. This can lead to production line slow-downs, or in worse cases, "reject parts" due to improperly assembled or machined components.
One method to counteract this issue is designing the jig using locating pins with a lead-in on the head. This can be in the form of an angled or tapered head, sphere, or bullet nose, and helps to center and ease the part onto the pin. Take care when incorporating a lead-in, though, as too much lead can result in a taller pin and create added difficulty in loading or unloading the workpiece.
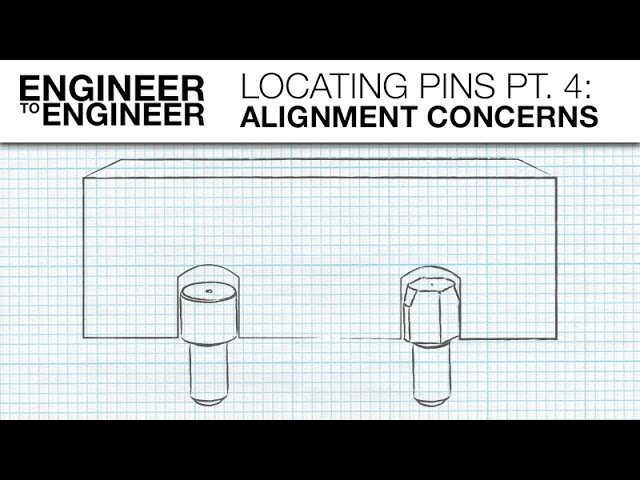
The other main way to avoid binding of a workpiece with a pair of locating pins is to use a dissimilar pair of pins, specifically a 2-way and a 4-way pin together. This is most commonly achieved through the use of a round pin and a diamond pin, which allows some radial play as a degree of freedom, helping to alleviate any lateral binding of the 2 pins with the workpiece.
With a better understanding of how to use pins with a lead-in, and dissimilar pin pairs, you should be well on your way to minimizing workpiece binding. If you need a refresher on 2-way and 4-way locating pins, check out Episode 2 of our locating pins series, and if you're interested in how to select materials and coatings for locating pins, tune in to our upcoming episode, Locating Pins Pt. 5: Material Selection.
=================================
Subscribe to our channel: bit.ly/Us2mJ6
BLOG: blog.misumiusa.com
Twitter: twitter.com/usa_misumi
G+: bit.ly/1nQPnvV
FB: facebook.com/misumi.usa
LinkedIn: linkedin.com/company/misumi
Locating Pins Pt. 4: Alignment Concerns | Engineer to Engineer | MISUMI USA
NEW CONFIGURABLE NAAMS COMPONENTS FROM MISUMI USA!
youtube.com/watch?v=FYi48fVdGfA
-~-~~-~~~-~~-~-
Locating Pins Pt. 4: Alignment Concerns | Engineer to Engineer | MISUMI USA
misumiusa.com
When working with and designing jigs or fixtures with locating pins, proper alignment is crucial to ensuring smooth operation and repeatable results. This episode will address a few of the most common solutions to alignment concerns for locating pins. If you're unfamiliar with the basics of locating pins and workholding concepts, check out the previous episodes in this series to get up to speed.
One of the biggest issues a new fixture designer encounters is binding of a part, where the way it is placed or removed from a pair of locating pins causes it to become stuck and out of alignment. This can lead to production line slow-downs, or in worse cases, "reject parts" due to improperly assembled or machined components.
One method to counteract this issue is designing the jig using locating pins with a lead-in on the head. This can be in the form of an angled or tapered head, sphere, or bullet nose, and helps to center and ease the part onto the pin. Take care when incorporating a lead-in, though, as too much lead can result in a taller pin and create added difficulty in loading or unloading the workpiece.
The other main way to avoid binding of a workpiece with a pair of locating pins is to use a dissimilar pair of pins, specifically a 2-way and a 4-way pin together. This is most commonly achieved through the use of a round pin and a diamond pin, which allows some radial play as a degree of freedom, helping to alleviate any lateral binding of the 2 pins with the workpiece.
With a better understanding of how to use pins with a lead-in, and dissimilar pin pairs, you should be well on your way to minimizing workpiece binding. If you need a refresher on 2-way and 4-way locating pins, check out Episode 2 of our locating pins series, and if you're interested in how to select materials and coatings for locating pins, tune in to our upcoming episode, Locating Pins Pt. 5: Material Selection.
=================================
Subscribe to our channel: bit.ly/Us2mJ6
BLOG: blog.misumiusa.com
Twitter: twitter.com/usa_misumi
G+: bit.ly/1nQPnvV
FB: facebook.com/misumi.usa
LinkedIn: linkedin.com/company/misumi
Locating Pins Pt. 4: Alignment Concerns | Engineer to Engineer | MISUMI USA