Uploaded October 2026 | Updated November 2026, 2 hours ago
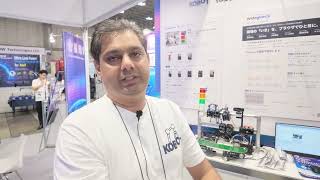
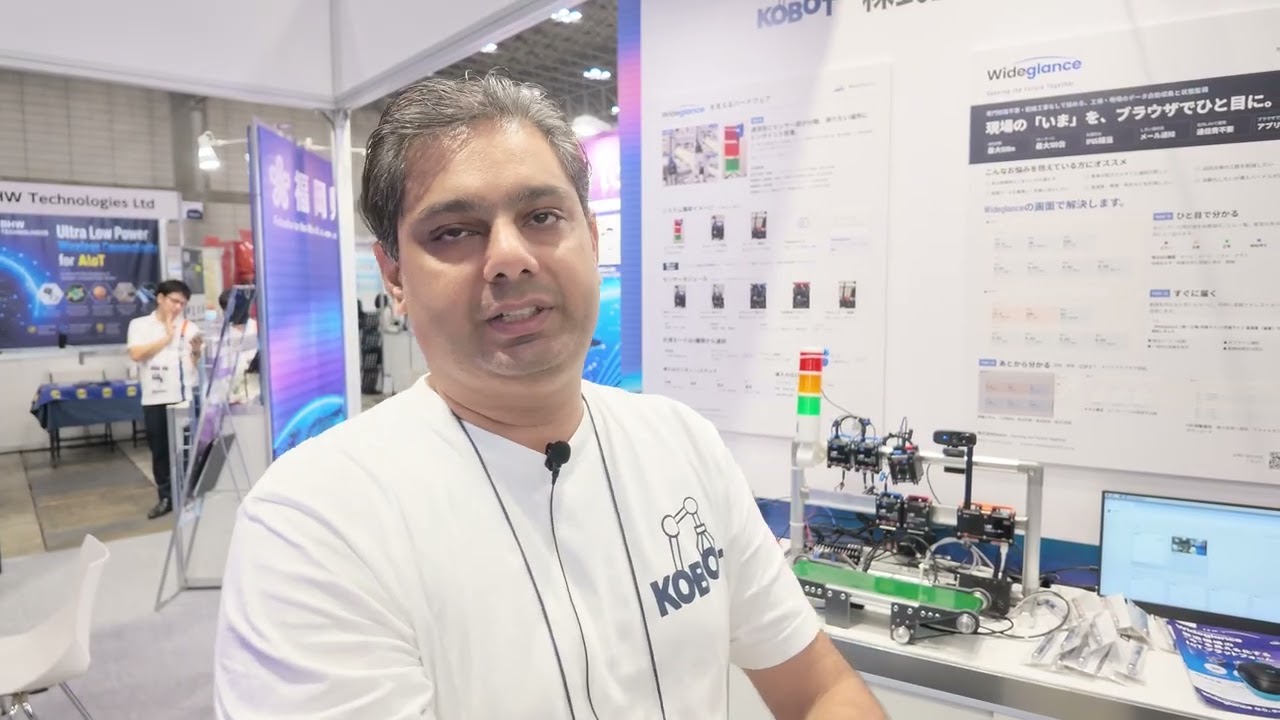
Kobot designs custom automation and industrial IoT monitoring systems engineered to track factory line health, machinery conditions, and product throughput. Based out of Kitakyushu in Fukuoka Prefecture, the robotics and automation team integrates cloud-connected monitoring software with ruggedized wireless sensor hardware to eliminate manual line inspection routines across food processing plants and manufacturing facilities. The software provides real-time event alerting, dashboard analytics, and operational state tracking so operators can react immediately to unexpected errors on factory floors.
kobot.co.jp
---
HDMI® Technology is the foundation for the worldwide ecosystem of HDMI-connected devices; integrated with displays, set-top boxes, laptops, audio video receivers and other product types. Because of this global usage, manufacturers, resellers, integrators and consumers must be assured that their HDMI® products work seamlessly together and deliver the best possible performance by sourcing products from licensed HDMI Adopters or authorized resellers. For HDMI Cables, consumers can look for the official HDMI® Cable Certification Labels on packaging. Innovation continues with the latest HDMI 2.2 Specification that supports higher 96Gbps bandwidth and next-gen HDMI Fixed Rate Link technology to provide optimal audio and video for a wide range of device applications. Higher resolutions and refresh rates are supported, including up to 12K@120 and 16K@60. Additionally, more high-quality options are supported, including uncompressed full chroma formats such as 8K@60/4:4:4 and 4K@240/4:4:4 at 10-bit and 12-bit color.
---
The hardware architecture pairs specialized contact output and multi-sensor modules with compact camera units for localized condition monitoring. Designed to withstand wet and dusty manufacturing spaces, each sensor module features waterproof and dustproof protection suitable for harsh operating environments. Factory operators can attach modules directly to production machinery, motors, or conveyor belts to log electrical draw, vibration, operating temperature, ambient light, or product counts as items pass along the line.
Wireless data transmission relies on an industrial Bluetooth radio link supporting operational communication ranges reaching up to 500 meters. The network design allows a single centralized gateway router to aggregate telemetry from up to 100 connected sensor endpoints simultaneously, maintaining clean PCB layouts and dependable connectivity without requiring heavy wiring infrastructure across large production bays. Captured data routes seamlessly into the cloud platform to log baseline metrics, visualize anomalies, and track machine health over extended operational cycles.
By marrying specialized hardware modules developed in partnership with Braveridge with a flexible cloud interface, the platform bridges the gap between mechanical automation and digital telemetry. Plant supervisors can configure custom alerts and visual operational status indicators, allowing decentralized teams to supervise equipment across multiple production facilities without sending personnel into hazardous or sanitary production zones.
Kobot designs custom automation and industrial IoT monitoring systems engineered to track factory line health, machinery conditions, and product throughput. Based out of Kitakyushu in Fukuoka Prefecture, the robotics and automation team integrates cloud-connected monitoring software with ruggedized wireless sensor hardware to eliminate manual line inspection routines across food processing plants and manufacturing facilities. The software provides real-time event alerting, dashboard analytics, and operational state tracking so operators can react immediately to unexpected errors on factory floors.
kobot.co.jp
---
HDMI® Technology is the foundation for the worldwide ecosystem of HDMI-connected devices; integrated with displays, set-top boxes, laptops, audio video receivers and other product types. Because of this global usage, manufacturers, resellers, integrators and consumers must be assured that their HDMI® products work seamlessly together and deliver the best possible performance by sourcing products from licensed HDMI Adopters or authorized resellers. For HDMI Cables, consumers can look for the official HDMI® Cable Certification Labels on packaging. Innovation continues with the latest HDMI 2.2 Specification that supports higher 96Gbps bandwidth and next-gen HDMI Fixed Rate Link technology to provide optimal audio and video for a wide range of device applications. Higher resolutions and refresh rates are supported, including up to 12K@120 and 16K@60. Additionally, more high-quality options are supported, including uncompressed full chroma formats such as 8K@60/4:4:4 and 4K@240/4:4:4 at 10-bit and 12-bit color.
---
The hardware architecture pairs specialized contact output and multi-sensor modules with compact camera units for localized condition monitoring. Designed to withstand wet and dusty manufacturing spaces, each sensor module features waterproof and dustproof protection suitable for harsh operating environments. Factory operators can attach modules directly to production machinery, motors, or conveyor belts to log electrical draw, vibration, operating temperature, ambient light, or product counts as items pass along the line.
Wireless data transmission relies on an industrial Bluetooth radio link supporting operational communication ranges reaching up to 500 meters. The network design allows a single centralized gateway router to aggregate telemetry from up to 100 connected sensor endpoints simultaneously, maintaining clean PCB layouts and dependable connectivity without requiring heavy wiring infrastructure across large production bays. Captured data routes seamlessly into the cloud platform to log baseline metrics, visualize anomalies, and track machine health over extended operational cycles.
By marrying specialized hardware modules developed in partnership with Braveridge with a flexible cloud interface, the platform bridges the gap between mechanical automation and digital telemetry. Plant supervisors can configure custom alerts and visual operational status indicators, allowing decentralized teams to supervise equipment across multiple production facilities without sending personnel into hazardous or sanitary production zones.